
While Cura offers many ways to increase the quality of your prints through the various features it offers, there’s a slight learning curve to knowing the capabilities of the slicer, knowing when to use which feature, and correctly adjusting the print settings accordingly to make the most out of the features you have enabled.
In this guide, we will explain the functionality of the top layers skin layers feature in Cura, discuss how you can find the optimal number of top surface skin layers to use, and go through the rest of the top surface skin parameters that allow you to configure the top surface skin layers in various ways.
Table of Contents
What Is the Top Surface Skin Layers Feature in Cura?
The top surface skin layers feature (part of top and bottom settings) in Cura allows you to separate a particular number of top layers from the rest in terms of the print settings that will be used for these layers, allowing you to customize the visible portion of the top layers in a way that would yield higher visual quality.
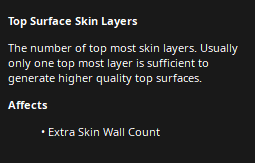
For instance, if the Top Layers value you’re using is 4, and the Top Surface Skin Layers value you’re using is 1, you will be able to configure the topmost layer, which is the one that will be the most visible from the outside, in a different way than the remaining 3 top layers in terms of factors such as line width, print speed, and pattern.

This way, you will be able to increase the quality of the topmost layer(s) through methods such as reducing the line width and print speed values without having to apply these changes to all of the top (and bottom) layers and avoid increasing print times needlessly for changes that would barely have an impact on how your printed part looks from the outside.

To put things into perspective, when slicing the calibration cube in the above example with 4 top layers and 0 top surface skin layers, using a top/bottom line width of 0.4 mm and a top/bottom speed of 30 mm/s, Cura gave us a time estimation of 35 minutes.

Once we decreased the top/bottom line width value to 0.3 mm and the top/bottom speed value to 20 mm/s, the time estimation went up to 39 minutes, an increase of 4 minutes in print time for higher-quality top layers.
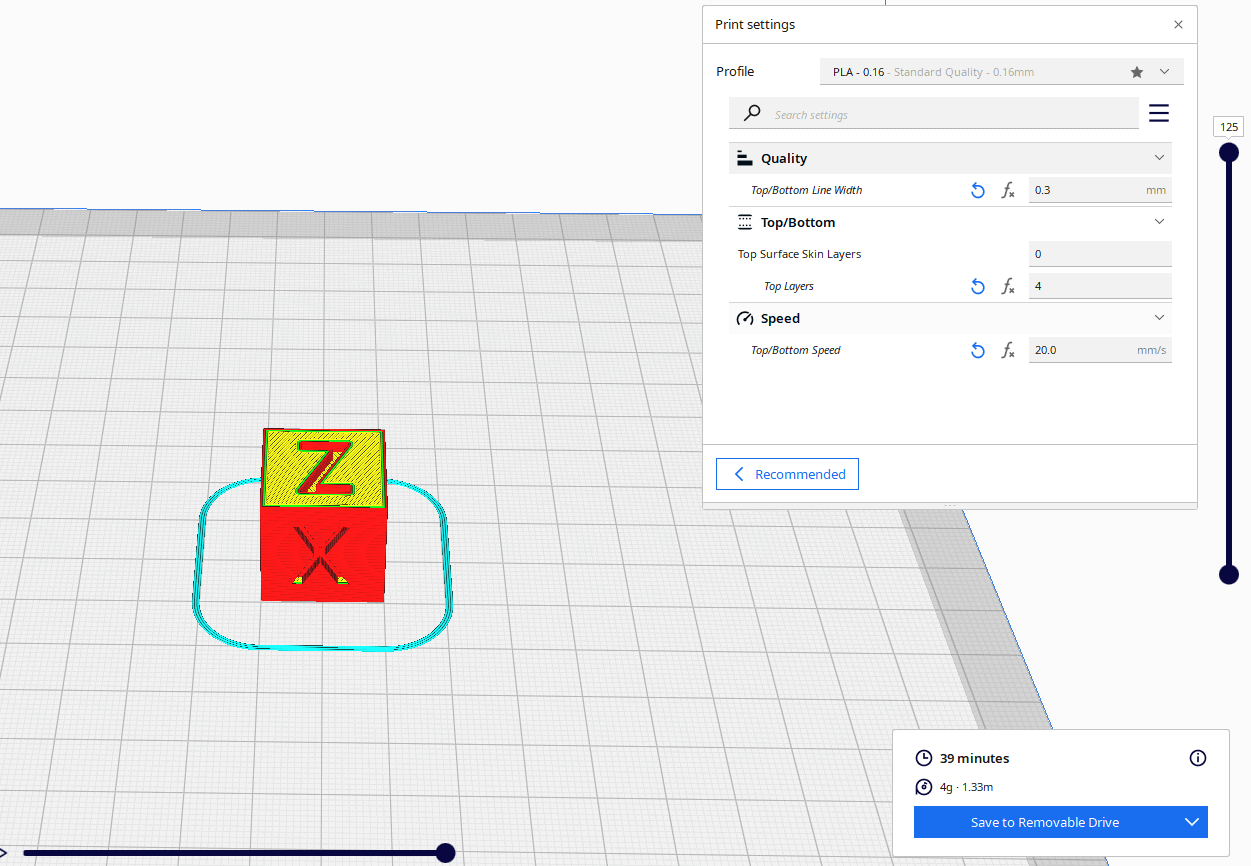
Next, instead of bringing the entire top/bottom line width and speed values down, we set the value of top surface skin layers to 1 with a top surface skin line width of 0.3 mm and a top surface skin speed of 20 mm/s (while leaving the rest of the top layers at their defaults of 0.4 mm line width and 30 mm/s speed), the time estimation went back down to 35 minutes again, effectively allowing us to obtain a top layer with higher visual quality for virtually no difference between print times versus the original example that used a higher line width and speed for the top layers.

While a difference of 4 minutes may seem small at first glance, these minutes (and even more if you print models that are wider on average than the 20 mm^3 calibration cube we have used for testing) will quickly add up to many hours of time saved in the long run, allowing you to squeeze in a lot more prints in the time that your 3D printer would otherwise have to spend unnecessarily, which makes top surface skin layers a tool that’s definitely worth adding to your configuration.
As a final example to show you how the print time savings will quickly add up, we have scaled the calibration cube up by 400% on the X and Y axes (80×80 from 20×20) to increase the time spent on the top and bottom layers and ran the same tests as we initially have.
Without the top surface skin layers feature active, Cura gave us a time estimation of 6 hours 13 minutes with a top/bottom line width value of 0.3 mm and a top/bottom speed value of 20 mm/s.

Next, we switched the top surface skin layers feature on, the same way as before, which brought Cura’s print time estimation down to 5 hours 1 minute, a whopping difference of 1 hour 12 minutes between the two prints!

Provided that you run such a print every day of the month, you will save around 36 hours a month in print time with this one simple adjustment, which would allow you to save on energy costs and reduce wear & tear to your 3D printer if nothing else.
How Many Top Surface Skin Layers Should You Use?
While the whole idea behind using the top surface skin layers feature is to configure enough of the top layers in a way that would result in an observable boost in visual quality, having a way too high number of such layers can end up with prolonged print times without yielding any significant improvement to quality.
In most cases, using a top surface skin layers value of 1 should be sufficient to create a high-quality top surface when combined with the correct top surface skin configuration based on our experiences, which is what Cura recommends doing by default as well since this will allow you to benefit from the top surface skin layers feature in the most efficient way possible, with the quality-to-time ratio diminishing for each added layer.
That being said, in cases where maximizing the visual quality of the topmost layer hasn’t been enough to reach the level you need, you can definitely go for a top surface skin layers value of 2, and while this won’t increase the overall quality of the top layers as much as the topmost layer did for the amount of time it takes, it will still give you a reasonable quality boost at the expense of an increased print time.
Finally, the benefits you gain out of using this feature diminish to a point where they will practically become unnoticeable with values higher than 2 and effectively create a scenario as if you weren’t using this feature at all due to the top surface skin layers making up the majority (or even the entirety) of the top layers, our recommendation would be to avoid going further than this.
Configuring the Top Surface Skin Parameters
The correct usage of the top surface skin parameters feature doesn’t end with determining the number of layers alone, as configuring the attributes of the specified layers is another critical part of ensuring that they can fulfill their duty of increasing the visual quality of the top surface.
Top Surface Skin Extruder
The top surface skin extruder parameter allows you to choose the extruder your 3D printer will use to print the top surface skin layers.

With a multi-extruder 3D printer, you can leverage this feature to either give the top surface a different color, or even distinct properties, such as using PLA for a better-looking finish or using TPU for a soft and rubbery top surface for a part that otherwise needs to be strong and hence printed with a material such as ABS.
Top Surface Skin Flow
The top surface skin flow parameter allows you to adjust the flow rate (extrusion multiplier) for the top surface skin layers.
While it shouldn’t become necessary to modify this value under normal circumstances, it can provide a quick band-aid fix in cases where you’re experiencing over-extrusion, under-extrusion, or excessive roughness problems explicitly when your 3D printer is printing the top surface.
Top Surface Skin Speed
The top surface skin speed parameter allows you to adjust the print speed for the top surface skin layers.

Reducing the top surface skin speed value to be lower than the top/bottom speed value is one of the primary ways to benefit from the top surface skin layers feature, as printing the topmost layer(s) slower will give them better visual quality, and make your part look better from the outside as a result.
In most cases, going for half the top/bottom speed value should be a good starting point, which you can build upon based on the results after you test it for the first time.
Top Surface Skin Acceleration
The top surface skin acceleration parameter allows you to adjust the acceleration for the top surface skin layers.
While modifying this value shouldn’t become necessary under normal circumstances, reducing the acceleration as your 3D printer prints the top surface can increase visual quality in cases where vibration affects the extrusion negatively and creates the infamous ghosting/ringing problem.
Top Surface Skin Jerk
The top surface skin jerk parameter allows you to adjust the jerk for the top surface skin layers.

Similar to acceleration, modifying the jerk value for the top surface shouldn’t be necessary for an increase in visual quality, but a slight increase (too much will lead to vibrations and possibly layer shifting) can come in handy for more consistent lines and fewer blobs on the surface and a slight decrease can remedy pre-existing vibration-related issues.
Top Surface Skin Line Width
The top surface skin line width parameter allows you to adjust the line width for the top surface skin layers.

Together with top surface skin speed, top surface skin line width is another one of the main parameters that will allow you to increase the print quality of the topmost layer(s) when you use a lower value than usual, as the top layer consisting of thinner lines will make it look a whole lot more smoother.
As a result, when configuring this value, we recommend getting the lines to be as thin as possible without causing under-extrusion, which would be roughly 60% of the nozzle size under normal circumstances, such as 0.24 mm for a 0.4 mm nozzle.
Top Surface Skin Pattern
The top surface skin pattern parameter allows you to adjust the pattern for the top surface skin layers, where you can choose between the Lines, Zig Zag, and Concentric options.

As the effects of your choice here will be purely cosmetic, feel free to pick out the one that makes the top surface look the best for your purposes.
Top Surface Skin Line Directions
The top surface skin line directions parameter allows you to adjust the direction of the lines when using the Lines and Zig Zag patterns by entering the angles of your choice in a comma separated format.

Similar to the top surface skin pattern parameter, your choice for the top surface skin line direction will also be purely cosmetic since it will only affect the topmost layer, meaning that you can feel free to go with the one that creates the best look.
Conclusion
The top surface skin layers feature in Cura is definitely a great tool to improve the visual quality of the top surface without prolonging print times way too much, as it practically allows you to make the changes that will be beneficial to the visual quality for the layers that will only be visible from the outside, without wasting time on the layers that you can’t see anyway.
That being said, as correct configuration, both when determining the number of layers that will be used and the slicer settings that the 3D printer will utilize when printing these layers, plays a vital role in ensuring that the top surface skin layers feature can do its job, we highly recommend double-checking everything to be able to benefit from this feature as best as possible.
Mike started his 3D printing journey with the Anet A8 when it first came out back in 2017, and has been obsessed with 3D printers ever since. Nowadays, he primarily uses his Ender 3 to print functional parts that make his life more convenient whenever possible.